The Sign-Off Comes Last: A Practical Three-Point Approval Routine for New Packaging Specifications
New packaging specifications often arrive with a sample, a specification sheet and an understandable desire to move quickly. The risk is that approval becomes a single visual check: the box looks right, the mailer closes, the tape sticks to the desk. That is not a test of how the pack will perform in a UK warehouse in February, on a pallet in a distribution centre, or in the back of a van during a wet delivery round.
TRM Packaging uses a simple three-point routine before a new specification is signed off. The initials are convenient: tape, rigidity and moisture. They are not a substitute for a full transit trial, but they give buyers and operations managers a repeatable way to challenge a sample before it becomes the standard pack.
Begin with tape, because tape is a system
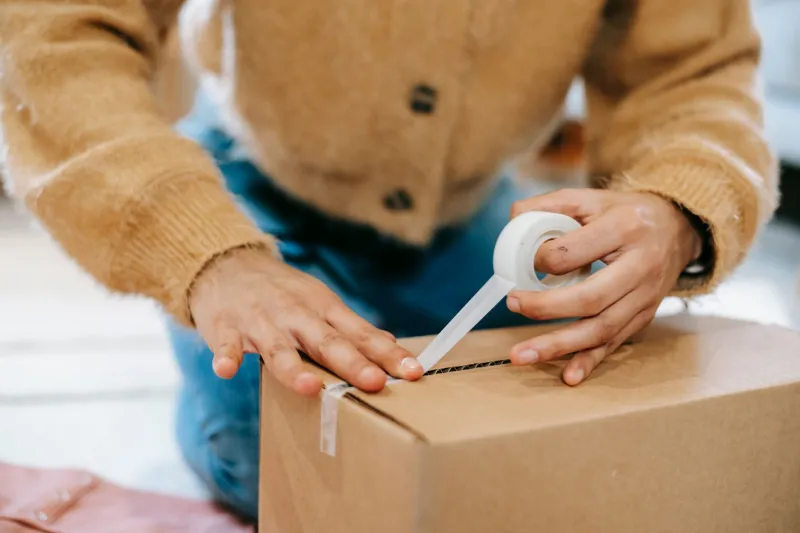
Tape is often treated as a consumable rather than a component. In practice, it is part of the closure system, and its performance depends on the board surface, the temperature, the applicator and the person applying it. A tape that performs well in a warm office may behave differently in an unheated warehouse or on a damp morning when condensation has settled on the board.
Ask the supplier for the adhesive type and the conditions it is designed for. Acrylic, hot-melt and water-activated tapes do not behave in the same way. Water-activated tape can form a strong bond with recycled board, but it requires the right equipment and a controlled amount of water. Pressure-sensitive tapes vary in initial tack and in their ability to tolerate dust or moisture on the board surface.
The practical test is straightforward. Condition a small number of packed samples in the area where they will actually be stored or staged, not in the meeting room. Apply the tape using the same dispenser and technique that the packing team will use. Leave the samples for a realistic period, then check for lift, curling and failure at the edges. Repeat the test after the pack has been handled and moved. If the tape only works when applied slowly by hand, it is not yet a production specification.
Also check the width and overlap. A narrow tape line may be adequate for a light mailer but insufficient for a heavy box that will be stacked. The approval question is not simply whether the tape sticks, but whether it continues to hold through the handling route.
Rigidity is a relationship, not a catalogue number
Board grade is usually expressed through technical values, and those values matter. But rigidity is not a property of the board alone. It is a relationship between the board, the product, the pack dimensions and the handling route. A box that performs well for a dense item may fail for a lighter but bulkier product that shifts in transit. A mailer that is rigid enough for a single item may bulge when the pack is stacked.
Test the sample with the actual product or a weighted dummy that matches its centre of gravity. Close the pack as it will be closed in production. Then handle it as the courier, pallet network or retail customer will handle it. Lift it by the corners. Stack it. Place it on a pallet and check for compression and bulge. Look at the score lines, the seams and the corners, because those are the points where failure usually begins.
Consider the route as well as the product. A parcel network involves repeated sorting and drops. A palletised delivery involves stacking and compression. A returns journey may involve opening and reclosure. If the pack is likely to be over-stacked in a van or storage area, the specification should account for that reality rather than assuming ideal handling.
This is also the point to challenge over-specification. A double-wall board may be justified for a heavy or fragile item, but it can add cost and material where a well-designed single-wall pack would suffice. The aim is not the strongest box available. It is the weakest pack that reliably protects the product through the intended route.
Moisture is a route-wide risk
Moisture damage is often associated with rain, but water is only one source. Condensation, damp floors, unheated storage, chilled vehicles and humid loading bays can all affect board strength and print quality. Recycled board is particularly sensitive to moisture uptake, and a pack that feels rigid in a dry room may soften after a night in a cold, damp environment.
Ask how the pack will be stored before dispatch and how it will be transported. If the route includes unheated storage or a long period in a trailer, test the sample under similar conditions where possible. Check the board for softening, the print for smudging and the tape for loss of adhesion. If the product itself is moisture-sensitive, consider whether a barrier liner, a moisture-absorbing sachet or a sealed inner bag is appropriate. Each addition has a cost and a recycling implication, so it should be justified by the route rather than added by habit.
For many UK operations, the most useful test is a simple one: condition a packed sample overnight in a cool, damp area and then handle it as normal. If the pack loses shape or the closure fails, the specification is not ready. If it performs well, the result gives the approval team evidence rather than assumption.
A short checklist before approval
Before signing off a new box, mailer or void-fill combination, the approval team should be able to answer the following questions:
- Has the tape been tested on the actual board surface and in the conditions the pack will meet?
- Has the pack been handled and stacked with the real product or a representative weight?
- Has the pack been conditioned in a cool or damp environment and checked for loss of rigidity?
- Has the closure been tested with the dispenser and technique the packing team will use?
- Has the pack been reviewed against the intended route, including parcel sorting, pallet stacking and returns?
- Has the specification been challenged for unnecessary material or cost?
Approval should be a staged decision, not a single signature. The sample that looks right on the desk is only the starting point. The specification that survives the tape test, the rigidity test and the moisture test is the one that belongs on the packing line.
TRM Packaging works with UK businesses to review packaging specifications against practical handling conditions. The three-point routine is deliberately short, but it is long enough to catch the failures that are expensive to discover after the first pallet has left the yard.