Cold-Weather Closure Assurance: Keeping Tape, Labels and Glue Reliable Across a UK Winter
Winter parcel failures rarely begin with a dramatic crush. More often, a seal that looked sound on the packing bench opens by a few millimetres in an unheated van, or a label lifts at one corner after a damp morning on a loading bay. By the time the parcel reaches the customer, the closure has become the weak point. For UK operations preparing for the November to February cycle, closure assurance deserves the same attention as box strength and void fill.
The closure is a system, not a single product
Tape, label adhesive and any glue used in assembly all depend on contact. Pressure-sensitive adhesives must wet out against the board surface before they can hold. That process is influenced by temperature, surface cleanliness, applied pressure and dwell time. A tape that performs well in a warm, dry packing room may behave differently on cold board in a dispatch area, or after several hours in an unheated courier vehicle.
The practical lesson is to treat the closure as a system. Changing tape without reviewing board storage, bench habits and label adhesive may simply move the failure from one part of the parcel to another.
Why cold warehouses and warm packing rooms create trouble
Cold conditions affect adhesives in two ways. First, lower temperatures can make the adhesive less able to flow into the microscopic texture of the board, reducing initial grip. Second, temperature changes can introduce moisture. Board stored in a cold area and brought into a warmer packing room may attract condensation before it reaches the bench. A faint film of water is enough to prevent a proper bond.
Unheated courier vans and overnight distribution hubs add a further stage. A parcel sealed at around 18–20°C may spend hours at much lower temperatures. The seal must therefore be judged not only on how it feels immediately after application, but on how it performs after a realistic cold interval.
Surface preparation and recycled-board dust
Recycled board is widely used for good environmental reasons, but it can shed more dust than virgin board. Dust is an adhesive's enemy because the tape may bond to loose particles rather than to the board fibres. A seal that looks neat can therefore be holding very little.
Good practice starts before the tape is applied. Store board flat, dry and wrapped where possible, and allow packs to acclimate before sealing. Avoid cutting or guillotining board immediately before closure if the process generates visible dust. Where dust is present on exposed flaps, a dry brush or lint-free cloth can help, but damp wiping should be avoided because it adds moisture to the surface.
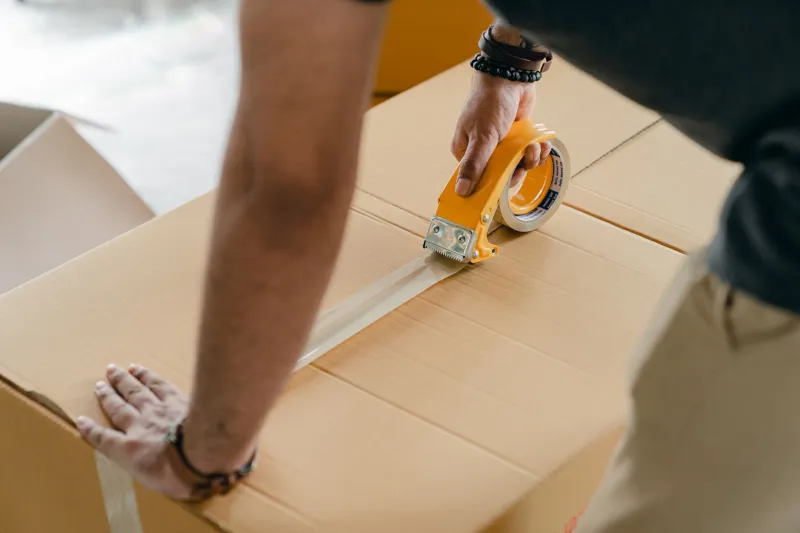
Compression pressure also matters. Hand smoothing alone may not be enough, particularly on recycled board. A tape dispenser with a pressure roller, or a separate hand roller used consistently, helps the adhesive achieve better contact. Briefing temporary staff on pressure and dwell time is as important as telling them which tape to use.
Choosing tape for lower temperatures
When reviewing tape specifications, ask suppliers for both application temperature and service temperature ranges. These are not the same thing. Application temperature refers to the conditions in which the tape is applied; service temperature refers to the conditions it must survive afterwards. A tape may cope with a cold journey but still be difficult to apply reliably on a cold bench.
Hot-melt and acrylic adhesives behave differently in the cold, and formulations vary between products. Low-temperature hot-melt grades may offer improved initial tack, while acrylic systems can have different long-term performance characteristics. Rather than assuming that a thicker tape is stronger, buyers should ask for evidence of adhesion to the board types actually used, including recycled board where relevant. Water-activated paper tape can also be worth reviewing where it suits the operation, but it is not a universal substitute for every closure.
Labels and glue: the overlooked closures
Labels are not decorative. They carry routing, compliance and customer information, and a lifted corner can cause scanning delays or a failed delivery. Low-temperature label adhesives are available, but performance still depends on the surface. Applying labels to damp board, or to board that has just moved from a cold store into a warm room, increases the risk of poor adhesion.
Where glue is used for pockets, inserts or assembly, check its open time and set time at the temperatures likely to be encountered. A glue that works comfortably at room temperature may become too viscous or set too slowly in a cold dispatch area. The same discipline applied to tape should be applied to these less visible closures.
A simple bench test for winter closures
A short, repeatable test is more useful than a last-minute switch to a heavier tape. It does not need laboratory conditions, but it should be consistent.
- Condition samples. Take the production tape, labels, glue and board. Keep a control set at room temperature and place a test set in a cool environment at around 2–5°C for at least two hours.
- Prepare realistic surfaces. Include clean board, dusty recycled board and, where condensation is a known issue, cold board brought into a warm room just until a faint bloom appears.
- Apply with consistent pressure. Use the same dispenser, roller or hand pressure for each sample, and allow the recommended dwell time before handling.
- Test after a cold interval. Peel tape at a shallow angle and record the failure mode. Board fibre tear is generally a better sign than clean adhesive release. For labels, check corners and edges for lift.
- Compare and record. If tape releases cleanly from dusty board, change the surface preparation or the tape specification. Repeat the test when the board supplier or tape batch changes.
Winter closure checklist
- Store board, tape and labels in dry, stable conditions and allow packs to acclimate before sealing.
- Ask suppliers for low-temperature application data for tape, labels and glue.
- Keep the packing bench clean and free from board dust; brush flaps only when necessary and avoid damp wiping.
- Use consistent pressure with a roller or dispenser rather than relying on hand smoothing alone.
- Run a cold-condition bench test before peak volumes and repeat it after any material change.
- Brief temporary staff on pressure, dwell time and surface preparation, not just tape selection.
- Review label adhesive if condensation or cold loading bays are routine.
The aim is not to find a single winter tape that solves every problem. It is to make closure performance predictable from November through February. A short bench test, realistic storage and a few disciplined habits at the packing bench will usually do more than a late change to a heavier or more expensive product.